


The 2UUL FS200 Joint X 200°C (50g) High-Temperature Solder Paste is an advanced micro-soldering alloy formulated specifically for high-stress BGA reballing, mobile CPU/GPU installations, and heavy-duty logic board power delivery circuits. Engineered with a specialized silver-bearing alloy profile melting at an exact threshold of 200°C, FS200 delivers superior mechanical shear strength, high thermal fatigue endurance, and vibration resilience far exceeding standard 183°C tin-lead or low-temperature alloys.
Engineered with spherical Type 4 (20–38 µm) micro-powder suspended in a low-residue, high-viscosity synthetic flux, 2UUL FS200 guarantees precise paste distribution through micro-stencils. It prevents aperture clogging, eliminates solder paste slump during heating, and ensures uniform, defect-free ball formation without bridging across dense 0.3mm–0.4mm pitch IC footprints.
Key Capabilities & Engineering Features
- High-Temperature 200°C Melting Point: Provides an ultra-durable thermal envelope, preventing joints from softening, fatiguing, or micro-cracking under intense processor thermal throttling and heavy gaming heat cycles.
- Engineered for High-Density Mobile CPUs: Specifically suited for primary system-on-chip (SoC) processors, baseband modems, and primary PMICs that demand high shear resistance and low thermal expansion.
- Precision Type 4 Particle Distribution (20–38 µm): Spherical micro-alloy formulation ensures consistent squeegee scraping through laser-etched stencils without voids, smearing, or missing balls.
- Anti-Slump & Anti-Bridging Viscosity: Maintains structural definition within stencil apertures under pre-heating stages, preventing molten solder from bleeding between tightly adjacent pads.
- Enhanced Wetting Chemistry: Fast-acting flux vehicle rapidly breaks down stubborn surface oxides on gold, nickel, and bare copper pads, ensuring low-resistance metallurgical bonding and bright, spherical solder balls.
- Non-Conductive, Clear Rosin Residue: Leaves high-impedance residue that prevents galvanic corrosion and parasitic current leakage. Cleans away completely using PCB cleaner or 99% isopropyl alcohol (IPA).
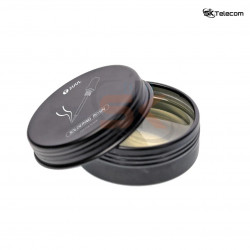
- Sealed 50g Workshop Packaging: Sturdy screw-top tub with an airtight inner foil seal to lock in flux moisture and prevent oxidation during bench storage.
Technical Specification Matrix
Parameter Profile | Specification Details |
Brand & Series | 2UUL Joint X Series |
Model Code | FS200 / GS200 |
Melting Point | 200°C (392°F) High Temperature |
Particle Size Grade | Type 4 (20–38 µm) |
Net Weight | 50g |
Flux Vehicle | High-Activity Synthetic Rosin / No-Clean Flux |
Recommended Hot-Air Temp | 300°C – 330°C (Nozzle setting with low-to-medium airflow) |
Storage Temperature | 0°C – 10°C (Refrigerated) for extended shelf life; equilibrate to room temp before opening |
Target Applications | Smartphone CPU/SoC reballing, baseband processor rework, power amplifier ICs, ruggedized PCB joints |
Step-by-Step CPU BGA Reballing Workflow
- Room Temperature Acclimation: Allow refrigerated containers to reach room temperature for 1 to 2 hours before opening to prevent atmospheric moisture condensation inside the jar.
- Pad Preparation: Wick residual solder from the CPU pads using high-grade desoldering braid and PCB cleaner until all pads are flat, bright, and free of carbonized flux.
- Align Stencil: Position a matching high-precision direct-heat or magnetic reballing stencil over the CPU, ensuring complete aperture alignment with zero gap.
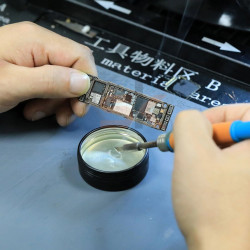
- Scrape Paste Smoothly: Apply a small bead of 2UUL FS200 and scrape across the stencil apertures with a stainless micro spatula at a 45° angle. Ensure every aperture is filled flush and clean off excess surface paste.
- High-Temp Reflow: Set your hot-air rework station to 300°C–320°C with low airflow (air volume 2–3). Direct the nozzle 1.5–2 cm perpendicularly above the stencil, circling evenly until all apertures reflow into bright, uniform spherical balls.
- Cool & Release: Allow the IC to cool for 20 seconds. Lightly spray PCB cleaner or IPA over the stencil, separate the chip, and complete a final clean to remove flux residue.
Package Contents:
- 1 × 2UUL FS200 Joint X 200°C High-Temperature Solder Paste (50g Tub)