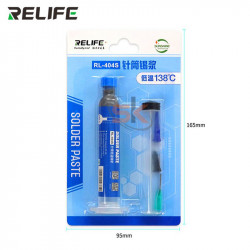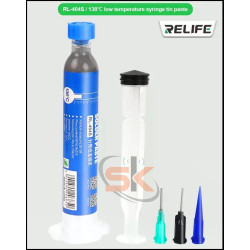



The FONEKONG 138℃ Melting Point Special Solder Paste for BGA Reballing (42g / Model FK-138 / FKGL42) is an ultra-low-temperature micro-soldering alloy paste engineered specifically for heat-sensitive mobile phone motherboard rework, sandwich board separation, and middle-frame interposer tinning. Formulated with an advanced Sn42Bi58 eutectic lead-free alloy and active no-clean flux carriers, this paste transitions to liquid state cleanly at 138°C (280.4°F), dramatically reducing thermal exposure on high-density smartphone logic boards.
By operating well below the standard 183°C and 217°C reflow thresholds, FONEKONG 138°C safeguards delicate internal structures against heat-induced motherboard blistering, inner CPU/baseband underfill blowout, and melted plastic FPC connectors. It is the premier choice for iPhone layered logic boards (iPhone X through newer flagship series) and multi-tier Android assemblies, producing bright, uniform solder spheres with minimal residue.
Key Engineering Features & Bench Advantages:
- Eutectic 138°C Low-Temperature Profile: Eliminates thermal stress during motherboard repair, preventing PCB layer separation, blister bubbles, and internal chip underfill eruption.
- Engineered for Double-Decker Logic Boards: The industry benchmark for reballing and re-bonding middle RF/logic board frames on split-board smartphones without disturbing interior baseband or CPU underfill layers.
- Micro-Fine Spherical Powder Matrix: Atomized alloy particles spread effortlessly across high-density BGA stencils (0.12mm–0.15mm) without aperture blockage, bridging, or tearing when removing the stencil.
- Non-Boiling & Anti-Tin-Bead Flux Carrier: Specially formulated organic flux vehicle prevents explosive paste boiling, micro-bead spatter, and void formation under direct hot air reflow.
- Superior Wetting & Clean Joint Formation: Rapidly strips surface oxides from copper and gold pads, creating bright, crack-free solder balls with low electrical resistance.
- Clear, Non-Conductive Post-Reflow Residue: Leaves minimal transparent, non-corrosive residue that washes away quickly with 99% isopropyl alcohol (IPA) and an ESD bench brush.
Technical Specification Matrix
Parameter Profile | Product Specification Details |
Product Model | FONEKONG FK-138 / FKGL42 Special Solder Paste |
Alloy Composition | Sn42Bi58 (42% Tin / 58% Bismuth Eutectic Lead-Free) |
Melting Temperature | 138°C (280.4°F) |
Net Weight | 42g Sealed Bench Pot |
Particle Size Grade | Micro-Fine Spherical Powder (Fine-Pitch BGA Ready) |
Flux Vehicle Classification | No-Clean, Low-Residue, Non-Corrosive Active Rosin |
Recommended Heating Sources | Heating Platforms / Preheaters, Hot Air Rework Stations |
Primary Bench Applications | Double-Decker Sandwich Board Rebonding, FPC Connector Soldering, Heat-Sensitive IC Reballing |
Bench Application & Usage Guide:
- Pad Preparation: Desolder old alloy from the interposer or IC pads using copper desoldering wick and flux. Thoroughly wipe the area with 99% IPA to remove residual carbonization.
- Stencil Loading: Align your precision BGA stencil over the middle frame or target IC. Spread a small portion of FONEKONG 138°C paste across the apertures using a flat scraper blade held at a 45° angle until every opening is evenly packed flush.
- Oil Equalization: For dense micro-arrays, lightly dab the top of the stenciled paste with a lint-free wipe to absorb excess surface oils before applying heat.
- Controlled Reflow Heating:
- With Heating Platform (Double-Decker Rebonding): Set your preheating bed to 170°C–185°C. The paste will reflow cleanly around 140°C–150°C, aligning the board halves without melting the inner CPU underfill.
- With Hot Air Torch: Set hot air station to 220°C–245°C with low airflow (20–30%). Hover the nozzle 1.5–2 cm above the stencil in continuous circular motions until all paste fuses into shiny, uniform spheres.
- Post-Reflow Cleanup: Allow the board to cool below 80°C. Clean remaining flux residue with an ESD brush and 99% IPA for a spotless, factory-inspected finish.