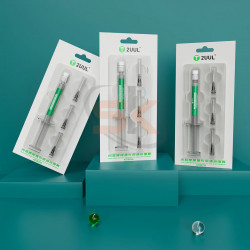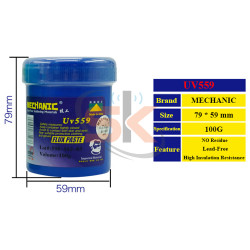



The 2UUL Joint X 158°C (50g) Low-Temperature Solder Paste is an advanced micro-soldering consumable engineered specifically for thermal-sensitive smartphone logic boards, layered motherboards (double-decker sandwich PCBs), and delicate BGA components. Designed to melt cleanly at an exact threshold of 158°C, this specialized formulation significantly lowers the required hot-air rework temperature compared to standard 183°C or lead-free 217°C alloys, eliminating board blistering, pad delamination, and underfill explosion around neighboring ICs.
Utilizing spherical Type 4 (20–38 µm) micro-particles suspended in an active, anti-slumping synthetic rosin flux, Joint X 158°C spreads smoothly across ultra-fine reballing stencils without clogging apertures or bridging microscopic pads. Its active flux chemistry dissolves surface oxide layers instantly, ensuring full, shiny solder spheres and high mechanical bond strength without brittle joints.
Key Capabilities & Engineering Features
- Low-Temperature 158°C Reflow Profile: Drastically reduces thermal stress on fragile multi-layer PCBs, double-decker iPhone/Android motherboards, and heat-sensitive sensors like Face ID and camera modules.
- Prevents Adjacent IC Damage: Lower thermal requirement prevents underlying underfill from boiling and shorting out surrounding components during CPU, baseband, and NAND reballing.
- Fine-Particle Type 4 Powder (20–38 µm): Spherical micro-alloy structure guarantees seamless stencil scraping, zero smearing, and uniform solder ball height across 0.3mm–0.4mm pitch grids.
- Balanced Anti-Slump Viscosity: Retains stencil aperture shape without collapsing or bleeding outward under pre-heat, preventing solder bead bridging and micro-shorts.
- High Wetting & Surface Deoxidation: Formulated with an active flux vehicle that breaks down copper, tin, and gold oxide films quickly, leaving bright, robust, and crack-resistant joints.
- Clean, Non-Corrosive Mild Residue: Leaves clear, high-impedance residue that causes no galvanic corrosion or electrical leakage across signal traces. Cleans off easily with PCB cleaner or 99% isopropyl alcohol (IPA).
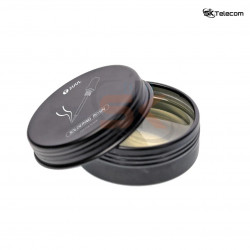
- Air-Tight 50g Workshop Packaging: Packaged in a heavy-duty screw-cap jar with an internal sealing barrier to lock in flux moisture and prevent premature paste drying on active repair benches.
Technical Specification Matrix
Parameter Profile | Specification Details |
Brand & Series | 2UUL Joint X Series |
Model Reference | FS183 / GS158 (158°C Formulation) |
Melting Point | 158°C (316°F) Low Temperature |
Particle Size Grade | Type 4 (20–38 µm) |
Net Weight | 50g |
Flux Vehicle | Low-Residue Synthetic Rosin / No-Clean Flux |
Recommended Hot Air Temp | 240°C – 260°C (Nozzle setting with low-to-medium airflow) |
Storage Temperature | 0°C – 10°C (Refrigerated) for extended shelf life; equilibrate to room temp before opening |
Primary Applications | Smartphone middle-frame reballing, sandwich motherboard joining, thermal-sensitive IC rework |
Step-by-Step Low-Temp BGA Reballing Workflow
- Temperature Stabilization: If stored refrigerated, allow the container to sit at room temperature for 1 to 2 hours before opening to prevent atmospheric moisture condensation.
- Pad Cleaning: Clean the IC pads or board interposer with a desoldering braid and PCB cleaner until pads are flat, bright, and free of old oxidized alloy.
- Mount Stencil: Align a precision direct-heat or magnetic stencil over the component, ensuring zero gap between the stencil foil and the pads.
- Scrape Paste Evenly: Apply a small bead of 2UUL 158°C paste and scrape across the stencil apertures with a stainless micro-spatula at a 45° angle. Ensure complete aperture filling and wipe away excess surface paste.
- Low-Heat Reflow: Set your rework station to 240°C–260°C with low airflow. Direct the nozzle 1.5–2 cm above the stencil, circling evenly until all apertures reflow into bright, uniform solder spheres.
- Cool & Release: Allow the assembly to cool for 15 seconds. Moisten the stencil lightly with PCB cleaner or IPA, lift the stencil smoothly, and brush away any remaining flux.
Package Contents:
- 1 × 2UUL Joint X 158°C Low-Temperature Solder Paste (50g Tub)