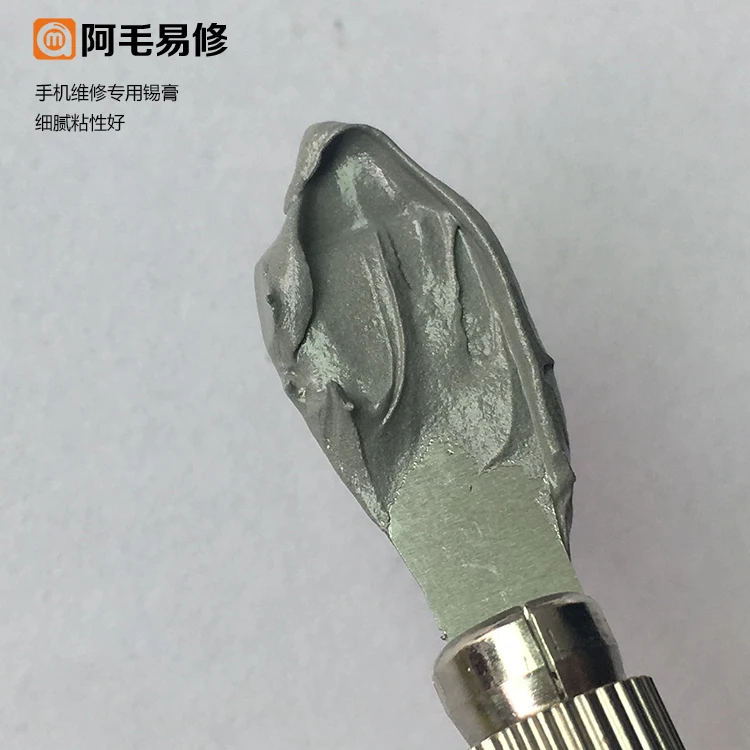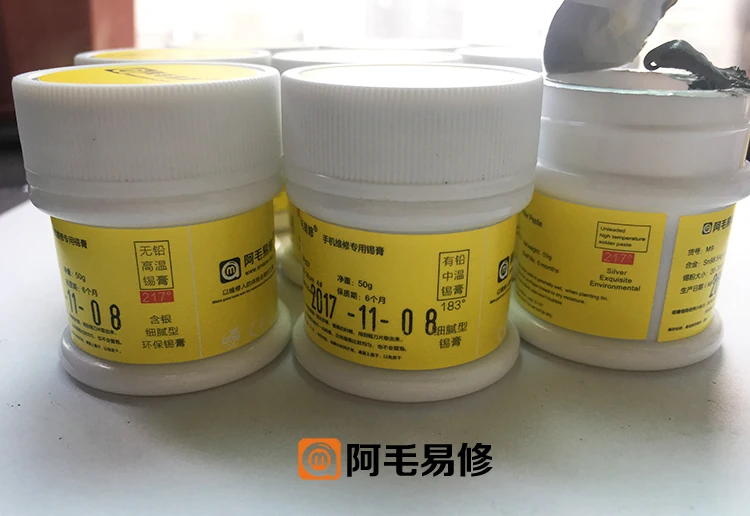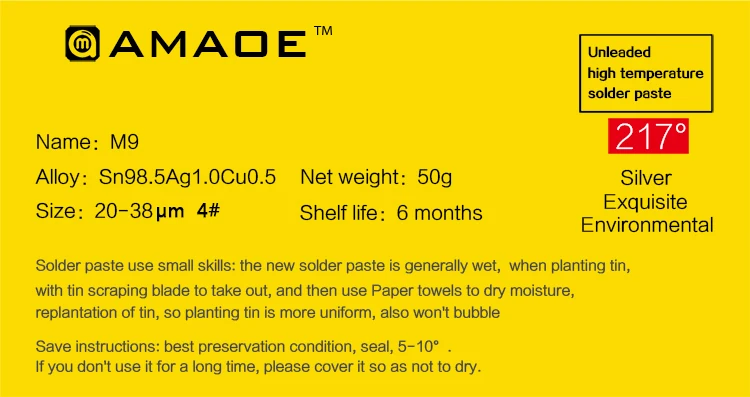

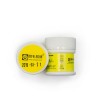


The Amaoe M13 (190°C) Medium-High Temperature Soldering Flux Paste is an advanced micro-soldering alloy paste formulated specifically for smartphone logic board rework, high-stress BGA reballing, and chip-level IC replacement. Engineered with a silver-doped metallurgy (Sn62.8/Pb36.8/Ag0.4) and active no-clean rosin flux carriers, M13 bridges the gap between conventional 183°C eutectic solder and high-temperature 217°C alloys. It melts cleanly at 190°C, delivering superior mechanical tenacity, exceptional electrical conductivity, and mirror-like joint glossiness.
The inclusion of elemental silver significantly enhances fatigue resistance and suppresses joint cracking under thermal shock and physical PCB flexing. Amaoe M13 eliminates false soldering, micro-void formation, and explosive flux boiling during reflow, making it the preferred formulation for master technicians performing heavy-duty CPU reballing, power-delivery IC mounting, and radio frequency (RF) transceiver repairs.
Key Engineering Features & Bench Advantages:
- Silver-Enriched Alloy (Ag 0.4%): Incorporates micro-alloyed silver to enhance tensile joint strength, reduce bulk resistance, and produce mirror-bright solder joints that resist drop-shock fractures.
- Calibrated 190°C Medium-High Thermal Range: Offers higher thermal resilience than 183°C pastes without subjecting sensitive smartphone motherboards to the damaging 217°C+ heat profile of standard lead-free alloys.
- No-Slump & Anti-Tin-Bead Flux Matrix: Designed to maintain its structural form under heat, preventing paste slumping, bridging, or erratic tin-bead dispersion across fine 0201/0402 micro-passives.
- Ultra-Fine 20–38µm Spherical Powder: High-density, uniform spherical micro-particles pass smoothly through ultra-fine 0.12mm–0.15mm BGA stencils without clogging apertures or tearing upon stencil removal.
- High Oxidation Resistance & Rapid Wetting: The built-in activated flux system quickly deoxidizes nickel, gold, and copper pads, creating full, uniform solder spheres during hot air reflow.
- Low-Residue, Non-Corrosive Post-Reflow Finish: Leaves minimal, clear, non-conductive residue that cleans up completely with 99% isopropyl alcohol (IPA) and an ESD brush.
Technical Specification Matrix
Parameter Profile | Product Specification Details |
Product Model | Amaoe M13 Medium-High Temperature Solder Paste |
Alloy Composition | Sn62.8 / Pb36.8 / Ag0.4 (Silver-Enhanced Formulation) |
Melting Point | 190°C (374°F) |
Particle Size Distribution | 20–38 µm (Micro-Fine BGA Spherical Powder) |
Flux Vehicle Classification | No-Clean, Low-Residue Active Rosin Matrix |
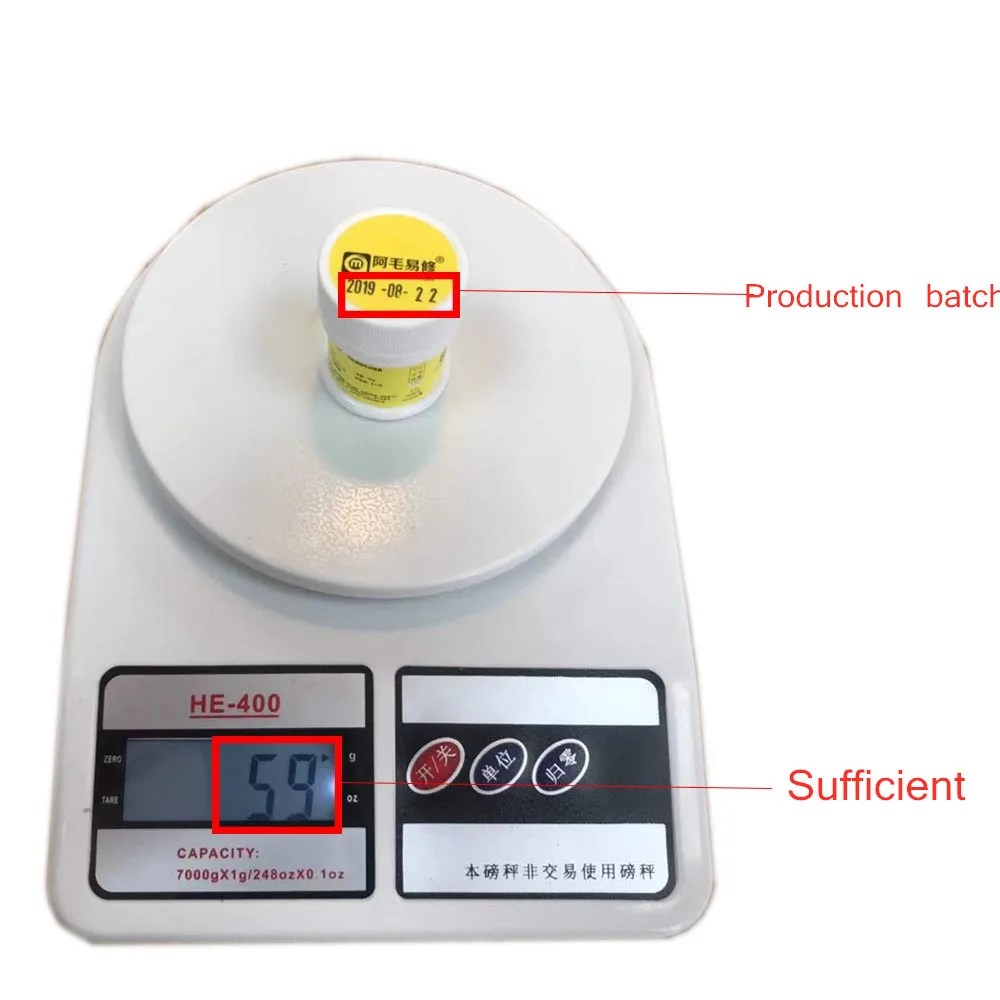
Standard Net Weight | 50g Airtight Screw-Cap Pot |
Recommended Heat Sources | Hot Air Rework Stations, Micro-Soldering Irons, Preheating Plates |
Primary Bench Applications | High-End Smartphone CPU Reballing, Power Management ICs (PMIC), Baseband & RF Transceiver Rework |
Bench Reballing & Application Guide:
- Pad Preparation: Use copper desoldering wick and flux to clear old oxidized solder from IC pads and logic board landing patterns. Thoroughly degrease the area using 99% IPA.
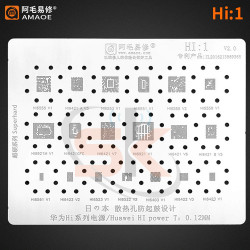
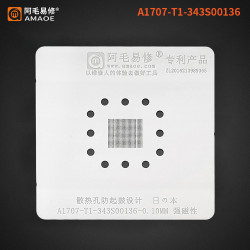
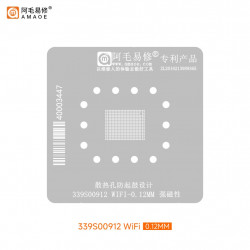
- Stencil Alignment & Paste Application: Fasten your precision Amaoe BGA stencil over the target chip. Spread a pea-sized bead of M13 paste evenly across the apertures with a flat scraper blade held at a 45° angle, ensuring every hole is filled flush.
- Oil Equalization: For high-density, fine-pitch BGA arrays, lightly dab the top surface of the stencil with a lint-free wipe to absorb excess surface flux oils and ensure uniform paste columns.
- Controlled Reflow Heating: Set your hot air rework station to 290°C–320°C with low airflow (25–35%). Hover the nozzle 1.5–2 cm above the stencil in continuous circular motions. As the alloy reaches 190°C, it will fuse into uniform, high-gloss spherical solder balls.
- Stencil Release & Inspection: Allow the stencil to cool for 5–10 seconds before popping the chip out. Apply a drop of liquid flux and reflow briefly under hot air for 3 seconds to achieve a mirror-bright, spherical factory finish.