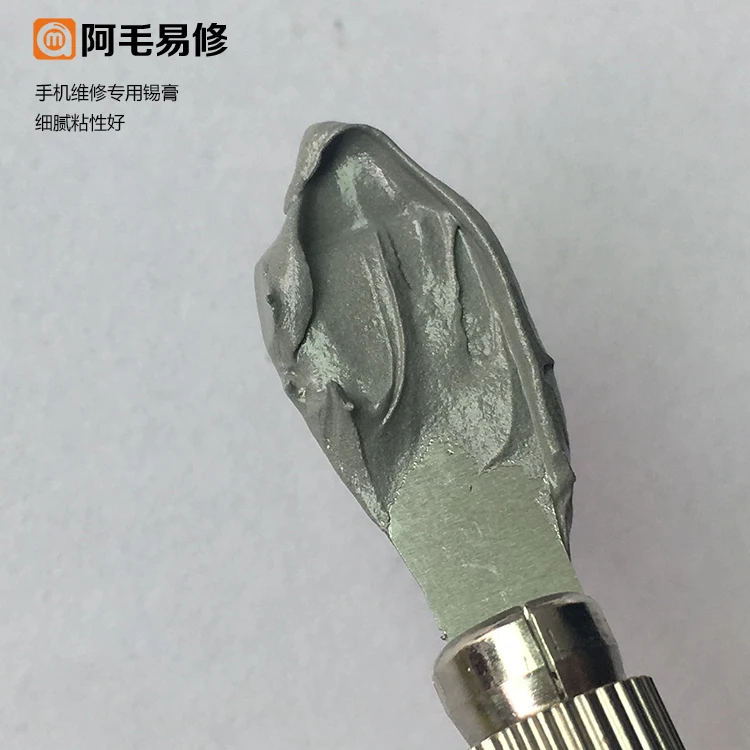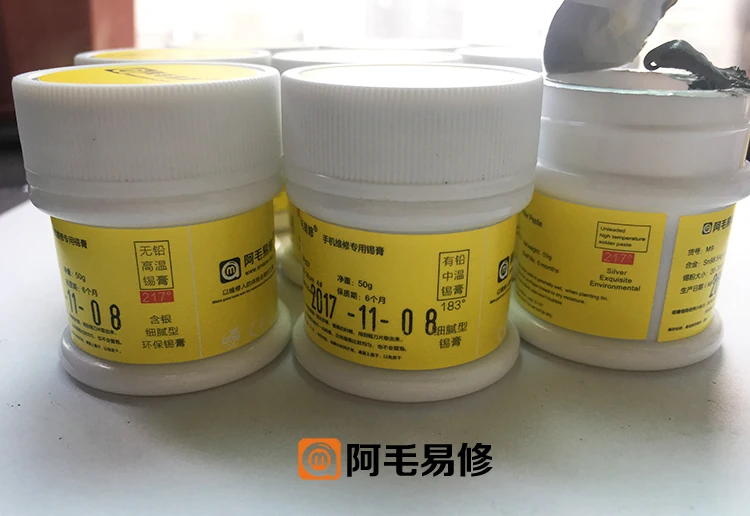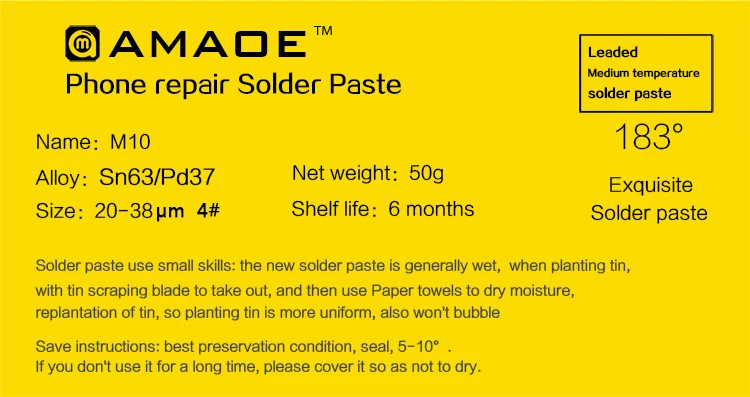

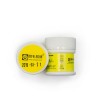
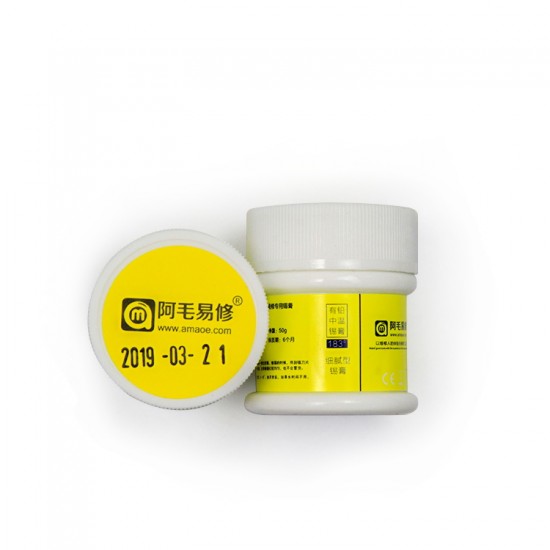

The Amaoe M10 (183°C) Medium-Temperature Solder Flux Paste is a benchmark micro-soldering alloy formulated specifically for smartphone motherboard repair, chip-level BGA reballing, and surface-mount device (SMD) rework. Engineered with a classic Sn63/Pb37 (63% Tin / 37% Lead) eutectic metallurgy and refined active flux carriers, the M10 melts sharply at 183°C, providing the ideal equilibrium between workable thermal safety and superior mechanical shear strength.
Unlike low-temperature bismuth alloys that can be brittle under physical board flexure, Amaoe M10 creates ductile, vibration-resistant, mirror-bright solder joints with exceptional electrical conductivity. Its finely atomized spherical micro-powder blends smoothly into fine-pitch stencil apertures, preventing dry solder joints, bridging, and explosive flux boiling during hot air rework on high-density smartphone logic boards.
Key Engineering Features & Bench Advantages:
- Eutectic 183°C Melting Point: Transitions instantly from solid to liquid phase without an intermediate pasty state, preventing cold solder joints caused by micro-movements during cooling.
- Superior Joint Fatigue Strength: The Sn63/Pb37 alloy matrix withstands physical drop impact, thermal expansion cycling, and motherboard flexing far better than low-temperature bismuth formulations.
- Ultra-Fine Micro-Powder Consistency: High-uniformity spherical solder particles glide smoothly through dense, fine-pitch stencils (0.12mm–0.15mm) without aperture clogging or tearing when the stencil is lifted.
- Anti-Tin-Bead & Low-Spatter Flux Vehicle: Advanced organic flux medium eliminates explosive solder paste boil-off, dramatically reducing stray tin beads and micro-bridging around tight 0201/0402 passives.
- Exceptional Wetting & De-Oxidizing Action: Fast-acting flux breaks through copper oxide films quickly, ensuring complete pad wetting and spherical ball formation with bright, uniform meniscus profiles.
- Non-Conductive, Clear Residue: Leaves minimal clear, non-corrosive residue around component pins that cleans off quickly with 99% isopropyl alcohol (IPA) and an ESD brush.
Technical Specification Matrix
Parameter Profile | Product Specification Details |
Product Model | Amaoe M10 Medium-Temperature Solder Paste |
Alloy Composition | Sn63/Pb37 (63% Tin / 37% Lead Eutectic Standard) |
Melting Point | 183°C (361.4°F) |
Powder Particle Size | Micro-fine Precision Spherical Powder (Fine-Pitch BGA Ready) |
Flux Vehicle Classification | No-Clean, Low-Residue, Non-Conductive Rosin Core |
Standard Packaging | 50g Airtight Screw-Top Bench Pot |
Recommended Heat Sources | Hot Air Rework Stations, Micro-Soldering Irons, Preheating Plates |
Primary Bench Applications | Smartphone CPU Reballing, NAND/EMMC Storage Swaps, Power IC & PMIC Soldering |
Bench Reballing & Application Guide:
- Pad Preparation: Desolder old alloy from the IC pad array using desoldering wick and flux. Thoroughly wipe the surface with 99% IPA to remove residual carbonization and underfill traces.
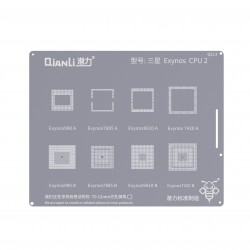
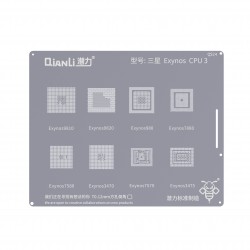
- Stencil Loading: Align your precision BGA stencil (e.g., Amaoe CPU/EMMC series) over the chip under magnification. Scoop a pea-sized portion of Amaoe M10 paste and spread it firmly across the mesh at a 45-degree angle with a flat scraper.
- Flux Oil Equalization: For ultra-fine pitch chips, lightly dab the freshly spread stencil surface with a lint-free wipe to absorb surface flux oils, ensuring crisp, uniform paste cylinders.
- Controlled Reflow Heating: Set your hot air rework station to 280°C–310°C with low airflow (25–35%). Hover the nozzle 1.5–2 cm above the stencil in continuous circular motions. As the paste liquefies at 183°C, watch the alloy draw into shiny, spherical balls in every hole.
- Separation & Final Polish: Allow the stencil to cool for 5 to 10 seconds. Release the chip gently. Apply a drop of liquid flux over the ball array and reflow briefly with hot air for 3 seconds to achieve a mirror-bright, spherical factory finish.