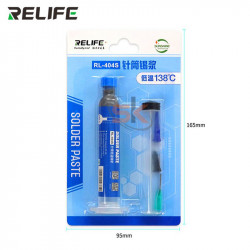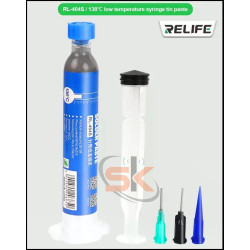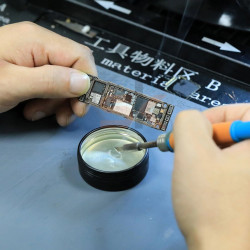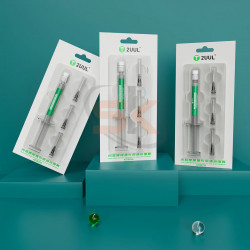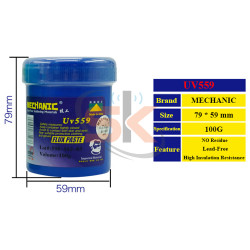



The 2UUL FS183 Joint X 183°C (50g) Solder Paste is an ultra-fine, professional micro-soldering solder paste engineered specifically for mobile device motherboard repair, CPU/NAND BGA reballing, and high-density SMD component rework. Built on a proven Sn63/Pb37 eutectic alloy ratio with an exact melting point of 183°C, FS183 transitions sharply from solid to liquid, eliminating plastic phases to produce bright, uniform, and crack-resistant solder joints.
Formulated with microscopic Type 4 powder spheres suspended in a high-activity, low-residue flux vehicle, 2UUL FS183 spreads smoothly across laser-cut stencils without clumping, slumping, or creating bridging between fine-pitch (0.3mm–0.4mm) solder pads. The specialized flux formulation cuts through heavy surface oxidation on nickel, gold, and bare copper pads, delivering high shear-strength joints and minimal non-corrosive residue for long-term board reliability.
Key Capabilities & Engineering Features
- Strict 183°C Eutectic Melting Point: Guarantees instantaneous melting and solidification during hot-air reflow, preventing cold joints and component displacement caused by uneven cooling.
- Fine-Grain Type 4 Particle Profile (20–38 µm): Ultra-fine, uniform spherical alloy particles allow effortless squeegee printing through micro-stencil apertures without voids or dry patches.
- Anti-Slumping & Anti-Bridging Chemistry: Maintains structural integrity inside the stencil apertures during pre-heat stages, preventing solder paste from overflowing between tightly grouped ball grids.
- Strong Wetting & Deoxidation Action: Actively dissolves surface oxide films on BGA pads and solder balls, ensuring low electrical resistance and high thermal conductivity across power and data lines.
- Non-Conductive, Clear Rosin Residue: Leaves a high-impedance, non-corrosive residue that will not cause current leakage or dendrite formation. Easily cleaned with standard PCB cleaner or 99% isopropyl alcohol (IPA).
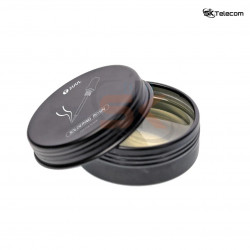
- Sealed 50g Workshop Packaging: Packaged in a sturdy, screw-top tub with an airtight inner seal to lock in flux moisture and prevent drying out between bench jobs.
Technical Specification Matrix
Parameter Profile | Specification Details |
Brand & Series | 2UUL Joint X Series |
Model Code | FS183 |
Alloy Composition | Sn63 / Pb37 (63% Tin, 37% Lead) |
Melting Point | 183°C (361°F) Eutectic |
Powder Particle Size | Type 4 (20–38 µm) |
Net Weight | 50g |
Flux Vehicle | Low-Residue Synthetic Rosin / Active No-Clean Flux |
Recommended Storage | 0°C – 10°C (Refrigerated) for extended life; bring to room temperature before opening |
Hot Air Rework Temp | 280°C – 310°C (Nozzle setting with low-to-medium airflow) |
Target Application | Smartphone CPU/Baseband/NAND BGA reballing, logic board trace bridging, PMIC rework |
Step-by-Step BGA Stencil Reballing Workflow
- Room Temperature Acclimation: If stored in a refrigerator, keep the jar sealed at room temperature for 1 to 2 hours prior to use to prevent condensation buildup inside the paste.
- Pad Bed Preparation: Clean the target BGA chip pads with a desoldering wick and PCB cleaner until all pads are flat, bright, and free of old oxidized alloy.
- Position & Clamp Stencil: Match the corresponding direct-heat or magnetic stencil to the chip pads and clamp it firmly to ensure zero gap between the stencil and IC surface.
- Scrape Paste Smoothly: Apply a small bead of 2UUL FS183 onto the stencil and scrape it across the apertures with a stainless micro spatula at a 45° angle. Ensure every aperture is filled completely and wipe off excess surface paste.
- Hot-Air Heating: Set your hot-air rework station to 280°C–300°C with low airflow (air speed 2–3). Direct the nozzle 1.5–2 cm above the stencil in continuous circular motions until all solder balls melt into uniform, shining spheres.
- Cool & Clean: Let the assembly cool for 15–20 seconds. Spray PCB cleaner or IPA over the stencil, carefully release the reballed IC, and gently brush away residual flux.
Package Contents:
- 1 × 2UUL FS183 Joint X 183°C Solder Paste (50g Tub)