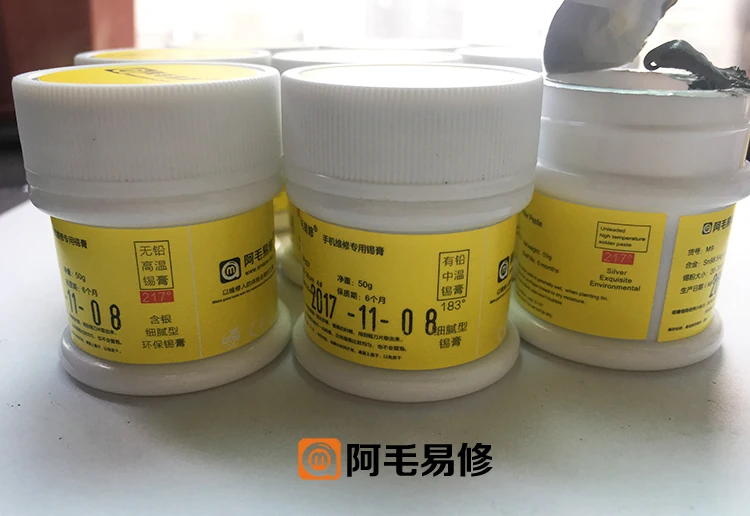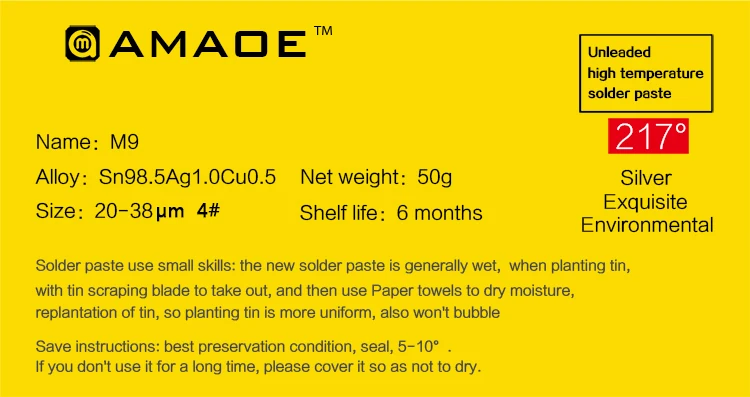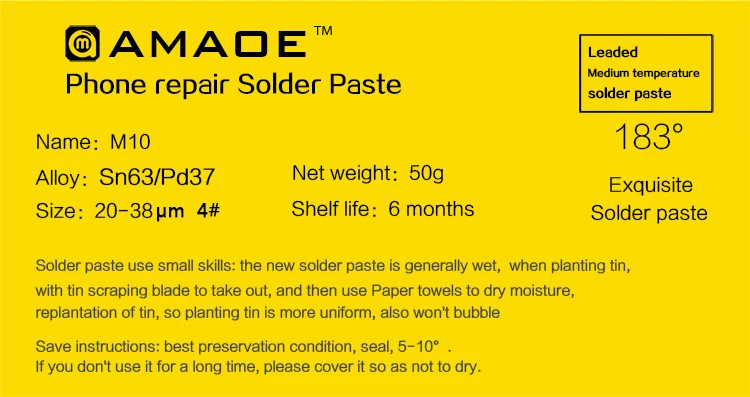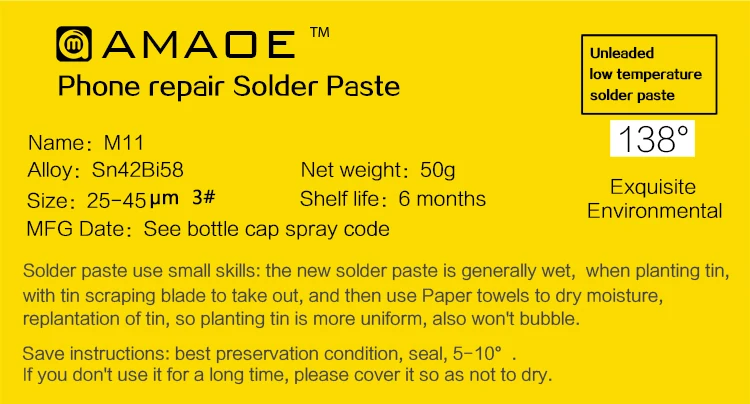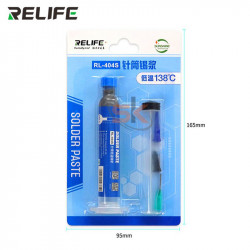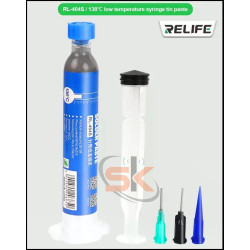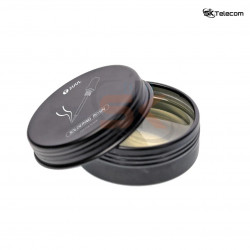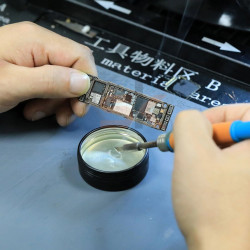

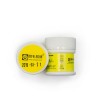


The Amaoe M11 (138°C) Low-Temperature Lead-Free Solder Flux Paste is an industrial-grade micro-soldering alloy paste formulated specifically for smartphone motherboard rework, multi-layer sandwich logic board repair, and heat-sensitive BGA/SMD component mounting. Formulated with a precise Sn42Bi58 (42% Tin / 58% Bismuth) eutectic alloy and high-activity, low-residue no-clean flux carriers, M11 liquefies cleanly at 138°C, dramatically lowering the thermal stress required during hot air and heating platform operations.
This low melting point solves one of the most persistent failure points on modern repair benches: thermal shock and component blistering. Standard SAC305 lead-free solder pastes demand rework temperatures upwards of 217°C–245°C, risking motherboard warping, CPU de-lamination, and melting adjacent plastic connectors (such as battery and FPC camera sockets). Amaoe M11 enables smooth, mirror-bright joints and reliable tin balling at a safe, controlled temperature profile.
Key Engineering Features & Bench Advantages:
- Eutectic 138°C Low-Temperature Melting Point: Minimizes board thermal exposure, virtually eliminating the risk of PCB layer separation, blister bubbles, and underfill blowout on adjacent chips.
- Optimized for Double-Decker Motherboard Rework: The industry standard choice for reballing and re-bonding middle RF/logic board frames on split-board smartphones (e.g., iPhone X through newer series, and stacked Android flagships) without melting interior baseband or CPU underfill.
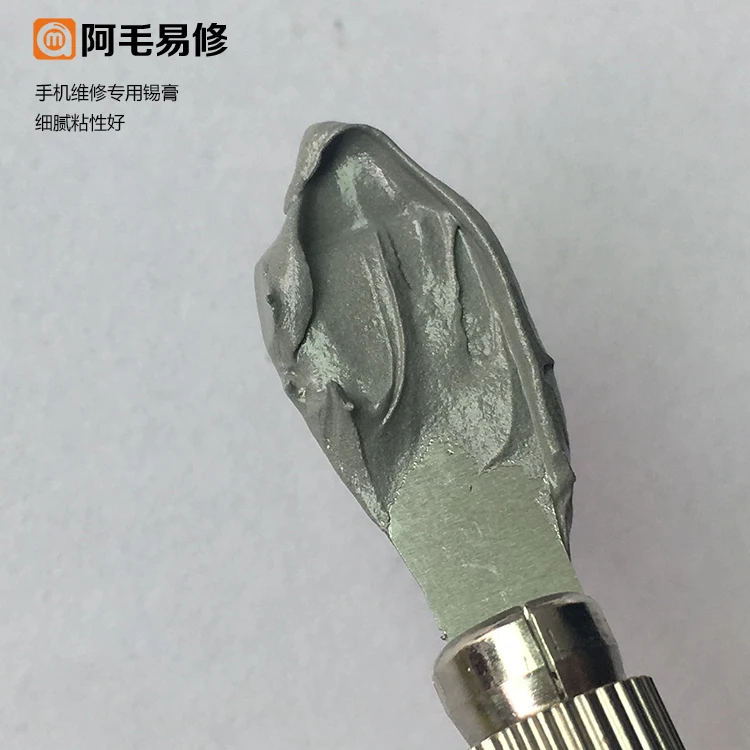
- Ultra-Fine Powder Consistency: Formulated with high-grade micro-particle spherical powder that spreads evenly across fine-pitch BGA stencils without clogging apertures or causing solder bridging.
- Non-Boiling & Anti-Tin-Bead Flux Matrix: Built-in high-performance organic flux vehicle prevents explosive paste boiling, micro-bead spatter, and void formation under direct hot air reflow.
- High Electrical Conductivity & Bonding Strength: Despite its lower melting point, the Sn42Bi58 alloy provides high mechanical shear resistance and low electrical impedance once fully cured.
- Low-Residue, Non-Corrosive Cleanliness: Leaves minimal, clear, non-conductive residue post-reflow that cleans off instantly using a standard ESD brush and 99% isopropyl alcohol (IPA).
Technical Specification Matrix
Parameter Profile | Product Specification Details |
Product Model | Amaoe M11 Low-Temperature Solder Paste |
Alloy Composition | Sn42Bi58 (Tin 42% / Bismuth 58% Eutectic Alloy) |
Melting Temperature | Exact 138°C (280.4°F) |
Particle Size Grade | Micro-fine Precision Spherical Powder (Fine-Pitch BGA Ready) |
Flux Vehicle Classification | No-Clean, Low-Residue, Non-Conductive Active Rosin |
Standard Packaging | 50g Airtight Screw-Top Bench Pot |
Recommended Heating Source | Heating Platforms / Preheaters, Hot Air Rework Stations |
Primary Bench Applications | Middle Layer Board Re-Bonding, FPC Connector Soldering, Heat-Sensitive IC Reballing |
Bench Application & Reflow Guide:
- Stencil Preparation: Ensure target IC pads or motherboard interposer frames are clean, flat, and free of old oxidized solder. Align your precision BGA stencil firmly over the pads.
- Even Scraping: Scoop a small bead of Amaoe M11 paste and spread it across the stencil using a flat scraper blade at a 45° angle. Scrape cleanly until each aperture is packed flush.
- Moisture & Oil Control: For ultra-fine pitch reballing, lightly dab the top of the stenciled paste with a lint-free wipe to absorb excess flux oils before applying heat.
- Controlled Reflow:
- With Heating Platform (Middle Layer): Set heating bed temperature to 170°C–185°C. The M11 solder balls will melt into unified joints around 140°C–150°C.
- With Hot Air Torch: Set hot air station to 220°C–250°C at low airflow (20–30%). Keep the nozzle moving circular 2cm above the stencil until all paste transforms into shiny, uniform spheres.
- Post-Reflow Cleanup: Allow the board to cool below 80°C. Clean remaining flux residue with a soft ESD brush and 99% IPA for a pristine, factory-grade inspection finish.